
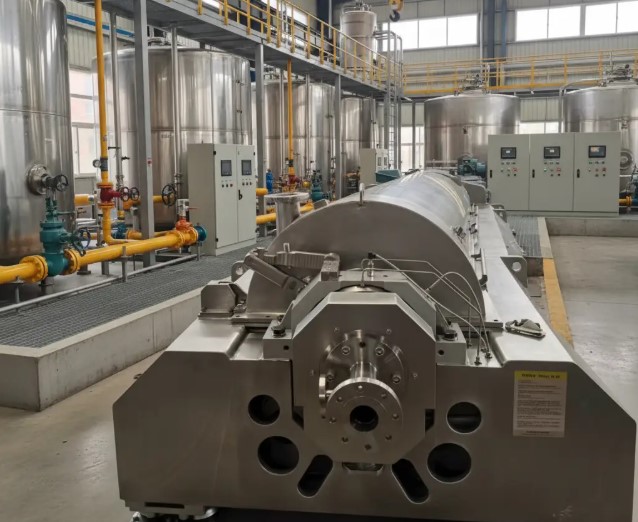
Industrial separation processes often involve demanding materials, continuous production schedules, and strict quality requirements. Standard equipment may not always provide the right combination of capacity, separation efficiency, durability, and process control for these applications.
Working with a specialized Centrifuge Machine Manufacturer can help companies select equipment around their actual production requirements. Shenzhou Machinery supplies centrifuge solutions for industrial processes where reliable solid-liquid or liquid-liquid separation plays an important role.
Why Do Some Industries Need Specialized Centrifuges?
Every industry handles different materials and operating conditions. Particle size, solids concentration, viscosity, temperature, chemical properties, and desired separation results can all affect centrifuge selection.
A specialized manufacturer understands these variables and can recommend equipment configurations that align with a particular process. This approach can also help businesses avoid investing in equipment that lacks the required performance or includes unnecessary features.
Food and Beverage Processing
Food and beverage manufacturers often need efficient separation during ingredient processing and product preparation. Centrifuges can support applications involving starch, oils, juices, dairy ingredients, and other process materials.
Equipment selection should account for hygiene requirements, material compatibility, cleaning procedures, and production capacity.
Manufacturers should also consider how the centrifuge integrates with upstream and downstream processing equipment.
Starch and Grain Processing
Starch production involves several separation stages where centrifuge technology can help remove solids and separate liquid phases.
Wheat, corn, and other grain-based processes may require equipment capable of handling specific particle concentrations and throughput levels.
A specialized supplier can evaluate the feed characteristics and recommend a configuration that supports the required separation process.
Chemical Manufacturing
Chemical plants often handle materials with challenging physical and chemical characteristics. Some processes involve corrosive liquids, abrasive solids, or strict temperature requirements.
Centrifuge construction materials and component selection therefore require careful consideration.
A specialized manufacturer can discuss corrosion resistance, process compatibility, operating parameters, and safety requirements before equipment selection.
Pharmaceutical Production
Pharmaceutical manufacturing requires careful control over processing conditions and product quality. Separation equipment may support processes involving active ingredients, intermediates, suspensions, and other materials.
Equipment selection should account for cleaning requirements, process consistency, material compatibility, and applicable production standards.
Manufacturers serving this sector need to understand the importance of controlled operating conditions and suitable equipment design.
Environmental and Wastewater Treatment
Wastewater treatment facilities handle large volumes of material containing suspended solids and other contaminants. Centrifuges can help separate solids from liquid streams during sludge treatment and related processes.
These applications often require continuous operation and dependable solids handling.
A specialized manufacturer can assess feed concentration, throughput, solids characteristics, and moisture targets when recommending equipment.
Mining and Mineral Processing
Mining operations frequently process abrasive slurries containing high concentrations of solid particles. Such conditions can place significant demands on centrifuge components.
Wear resistance and robust construction become important considerations in these environments.
The manufacturer should evaluate particle characteristics, slurry concentration, processing volume, and expected operating hours before selecting the appropriate equipment.
Drilling and Oilfield Applications
Drilling operations generate fluids containing solids that require effective separation. Centrifuge systems can help process drilling fluids and manage solid-liquid separation during field operations.
These applications may involve abrasive materials, demanding operating environments, and limited installation space.
A specialized supplier can help determine suitable equipment characteristics based on the drilling process and fluid composition.
Biotechnology and Biological Processing
Biotechnology facilities may use centrifugation during various stages of biological material processing. Separation requirements can vary significantly depending on the material and production stage.
Gentle handling, controlled operating conditions, and suitable equipment configuration may matter more than maximum throughput in certain applications.
Discussing the complete process with a manufacturer can help identify appropriate operating parameters and equipment features.
Pulp and Paper Manufacturing
Pulp and paper facilities manage large quantities of fiber, water, and process solids. Separation equipment can support different stages of material recovery and process-water management.
The abrasive nature of some process streams can influence component selection and maintenance requirements.
A manufacturer with industrial application experience can help match equipment construction and capacity to the production environment.
Edible Oil and Oil Processing
Oil processing involves separation tasks that may require equipment designed for specific liquid and solid characteristics. Centrifuges can support clarification and phase separation in suitable applications.
Factors such as density differences, viscosity, temperature, and desired product quality influence equipment selection.
Specialized technical guidance can help processors choose a centrifuge that fits their production conditions.
What Should These Industries Look For?
Although applications differ, several factors deserve attention when selecting an industrial centrifuge.
Companies should evaluate:
- Processing capacity
- Separation requirements
- Feed material characteristics
- Construction materials
- Wear resistance
- Automation and controls
- Maintenance requirements
- Spare-parts availability
- Safety features
- Technical and after-sales support
Evaluating these factors together provides a better basis for comparing equipment than looking at purchase price alone.
When Should You Choose a Specialized Manufacturer?
A specialized manufacturer can provide particular value when the process involves unusual materials, demanding operating conditions, continuous production, or strict separation targets.
It also makes sense to seek specialized support when a standard catalog machine does not clearly match the application’s requirements.
Detailed discussions about feed characteristics, production goals, installation conditions, and maintenance expectations can lead to a more suitable equipment choice.
How Shenzhou Machinery Supports Industrial Applications
Shenzhou Machinery focuses on centrifuge equipment for industrial separation processes. Its product solutions can serve applications where businesses need equipment matched to specific process conditions.
When evaluating a supplier, buyers should discuss their complete application rather than selecting a machine based solely on general capacity figures. Technical communication before ordering can help clarify equipment configuration, operating requirements, and expected performance.
Final Thoughts
Many industries can benefit from specialized centrifuge technology, including food processing, starch production, chemical manufacturing, pharmaceuticals, wastewater treatment, mining, drilling, biotechnology, pulp and paper, and oil processing.
The right equipment depends on the material, separation objective, production volume, and operating environment. Companies should therefore work with a manufacturer that understands their application and can provide suitable technical guidance.
Choosing the right centrifuge at the planning stage can support reliable operation, manageable maintenance, and consistent separation performance throughout the equipment’s service life.